
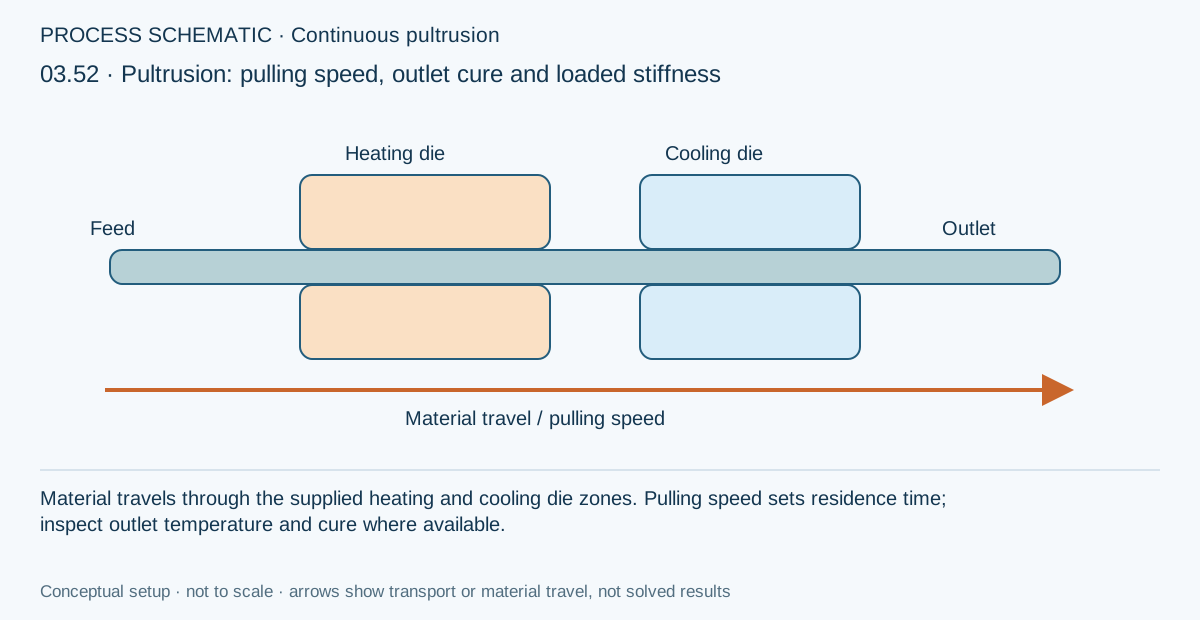
In a pultrusion study, pulling speed connects a position along the die to the time experienced by a moving material section. The exercise uses that relationship to examine residence time, heating and cure, with a structural comparison only where the selected simulation supports that transfer.
Open this exercise in Workbench
Prepare the baseline
Check the die length, inlet state, pulling speed and boundary stations before changing between length and time views. Keep the intended coordinate basis fixed while comparing speeds. Record the computed outlet state for each run; a prescribed die temperature is not an imposed core temperature or a guarantee of complete cure.
Worked procedure
1. Trace the 1.6 m die, 0.1 m/min pulling velocity and the shared laminate feeding the structural load. Moisture is disconnected.
2. Run the active simulation. Record residence time, outlet core temperature, outlet cure, reported structural coupling state and axial strain under Nx = 50,000 N/m.
3. With Length selected, compare 0.05, 0.1 and 0.2 m/min. Rerun the whole simulation each time; tabulate residence time, cure and strain.
4. Use the reported coupled stiffness and temperature to explain changes. Compare only runs with valid solver results; incomplete cure is a process outcome, not a successful manufacturing qualification.
Review checkpoints
Residence times are 32, 16 and 8 min for the three speeds.
The structural result uses the solver-reported coupled state; do not substitute assumed room-temperature cured properties.
Separate thermal expansion from mechanical strain and cure-dependent stiffness.
Model limits
Hypothetical teaching process using existing T700/epoxy laminate properties and illustrative cure parameters, not a calibrated pultrusion recipe. Constant-speed moving section; no axial conduction, impregnation, leakage, die thermal mass or pulling-force prediction. Use Thermal Run, not batch-cycle optimization. Sequential outlet-state structural screening under a prescribed resultant; no pulling force, die friction, impregnation or load feedback into the thermal solution.
Interpret the comparison
Explain the process result using the reported residence time and surface/core histories. For coupled variants, also record the actual state and stiffness passed into the structural calculation. Separate changes caused by section thickness or applied load from changes caused by cure, and do not infer an acceptable production speed without calibrated requirements.
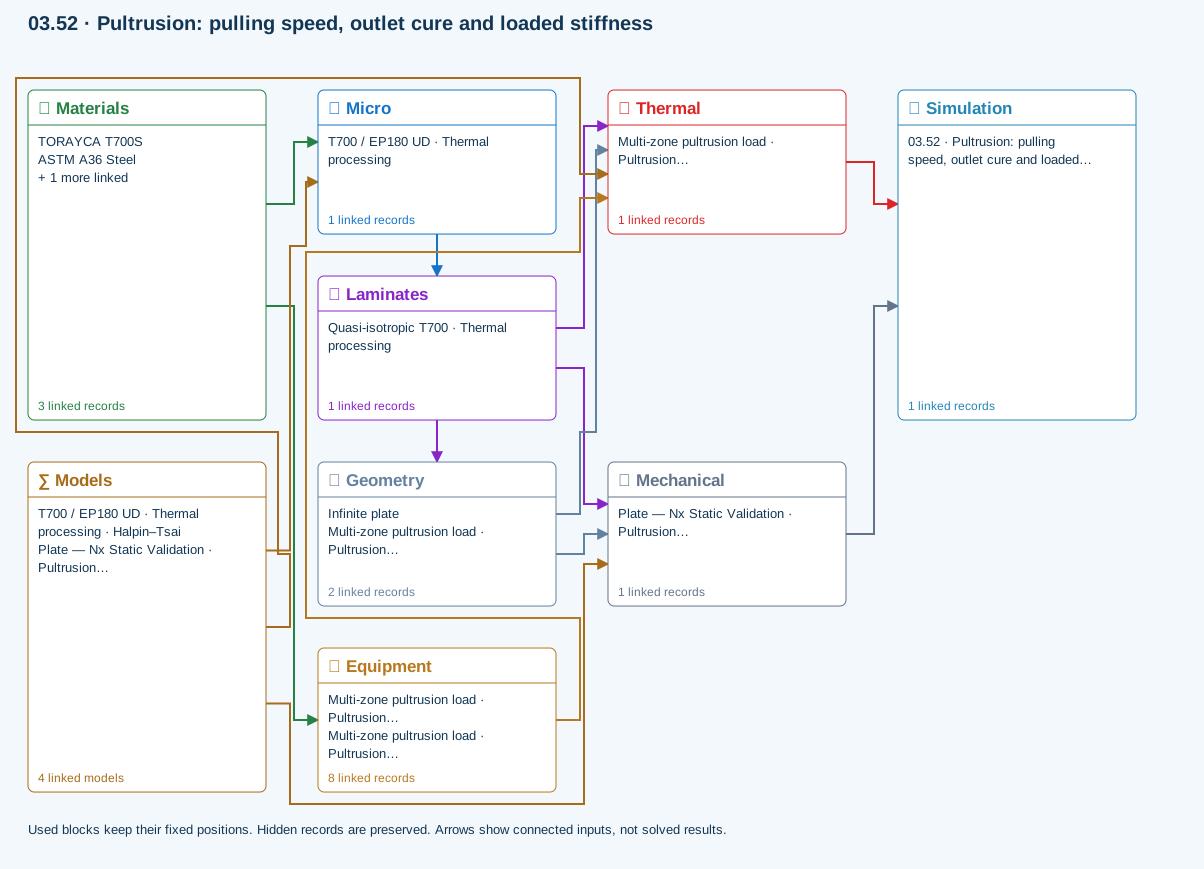
How information passes between models
Micro → Laminates: Predicted ply stiffness, strength, density and expansion properties.
Laminates → Geometry: Ply angles and thicknesses, stiffness, mass and ply properties.
Materials → Equipment: Constituent stiffness, strength, density and thermal / moisture properties.
Materials → Micro: Constituent stiffness, strength, density and thermal / moisture properties.
Mechanical → Simulation: SIMULATION selects this case and its analysis model; the case owns its applicable cycle and input references.
Laminates → Mechanical: Ply angles and thicknesses, stiffness, mass and ply properties.
Geometry → Mechanical: Part shape and dimensions, thickness or section definition, and model-specific geometric inputs. Each selected case consumes only the dimensions its model supports.
Thermal → Simulation: SIMULATION selects this case and its analysis model; the case owns its applicable cycle and input references.
Laminates → Thermal: Ply angles and thicknesses, stiffness, mass and ply properties.
Geometry → Thermal: Part shape and dimensions, thickness or section definition, and model-specific geometric inputs. Each selected case consumes only the dimensions its model supports.
Equipment → Thermal: Linked lasers, IR/UV lamps, heaters, coolers and molds: dimensions, radiant power or prescribed temperature / heat flux, contact conductance, body and surface materials. Each boundary keeps its own placement, side and exposure.
Models → Micro: Applied model assignment: Halpin–Tsai. Model parameters and formulation are used by Micro.
Models → Mechanical: Applied model assignment: CLT · Linear static with failure indices. Model parameters and formulation are used by Mechanical.; Maximum stress
Models → Thermal: Applied model assignment: 1D pultrusion thermal cure. Model parameters and formulation are used by Thermal.
Further reading and evidence
- Connect a simulation
- Edit laminate materials, angles and thicknesses
- Run and review a model
- Cure exotherm and evolving modulus
- Enter a process cycle and boundary conditions
- Connected inputs and result freshness
- Review effective properties
- Apply symmetry and balance
- Related case study: NASA process cure
Review the recorded validation scope. Retain the original inputs and solver notices with the results. Representative teaching data are not design allowables.
References and source sections
References are retained with the formulations they support. Software instructions describe implementation scope; a cited source does not establish independent validation of a CDS calculation.